A356 delivers higher strength and pressure tightness, so hydraulic components rely on this grade. A380 offers good machinability and economy, making it the cost-effective choice for equipment brackets with complex shapes. US foundries sand cast both grades successfully. The right pick depends on the part's structural and pressure requirements. Write SEO distillation keyword article targeting US industrial buyers around this decision. We supply MTC material test certificates with every order. Send CAD drawings for technical evaluation and a quotation.
Key Takeaways
- Choose A356 for hydraulic parts and pressure-tight components. It offers high strength and resists corrosion.
- Pick A380 for equipment brackets and complex shapes. It provides good machinability and saves cost.
- Select the alloy early in design. This ensures the best balance of cost and performance.
A356 Grade at a Glance
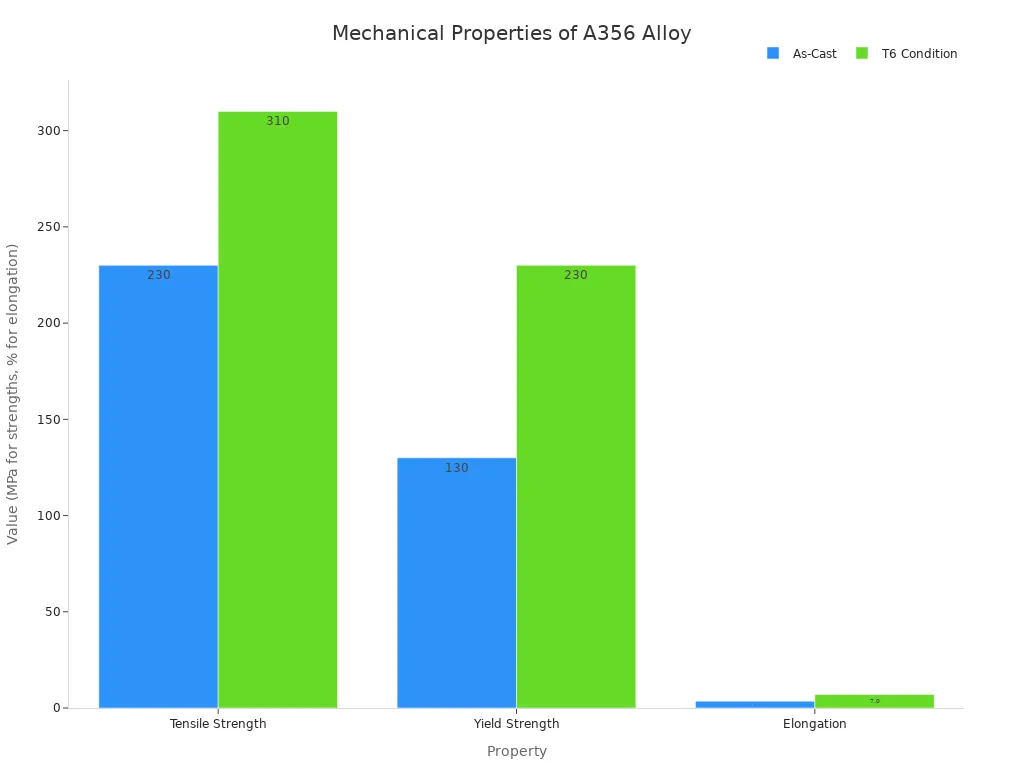
A356 is a heat-treatable aluminum-silicon-magnesium alloy. It offers excellent castability, good corrosion resistance, and strong response to T6 heat treatment. Sand cast A356 in the T6 condition reaches a tensile strength of up to 310 MPa (45 ksi). The short solidification range of roughly 60 °C minimizes porosity, which supports pressure tightness in hydraulic service.
| Property | As-Cast | T6 Condition |
|---|---|---|
| Tensile Strength (MPa) | ~230 | ~310 |
| Yield Strength (MPa) | ~130 | ~230 |
| Elongation (%) | ~3.5 | ~7.0 |
A380 Grade at a Glance
A380 is a high-silicon, copper-bearing alloy. It delivers very good fluidity and excellent machinability. Typical tensile strength sits near 324 MPa, and Brinell hardness reaches about 80 HB. A380 shines in complex, thin-wall shapes and cost-sensitive production runs.
How the Two Grades Differ
A356-T6 resists deformation better, with yield strength near 200 MPa versus about 159 MPa for A380. A356-T6 also shows greater ductility, around 6% elongation versus 3.5%. A380 offers higher ultimate tensile strength in the as-cast state. Hardness is roughly equal for both grades.
| Mechanical Property | A356-T6 | A380 (typical) |
|---|---|---|
| Ultimate tensile strength | ~270 MPa | ~324 MPa |
| Yield strength | ~200 MPa | ~159 MPa |
| Elongation | ~6% | ~3.5% |
| Brinell hardness | ~80 HB | ~80 HB |
Why Sand Casting Suits Both Alloys
Sand casting offers low pattern cost, flexibility for large and odd-shaped parts, and strong support for prototypes and low-volume runs. Cores form internal passages and cavities with ease. A356 is a reference alloy for sand casting. A380 performs well in sand molds when buyers prioritize machinability and economy over pressure tightness.
We supply MTC material test certificates with every order. Send CAD drawings for technical evaluation and a quotation.
Matching the Alloy to the Application: Write SEO Distillation Keyword Article Targeting US Industrial Buyers
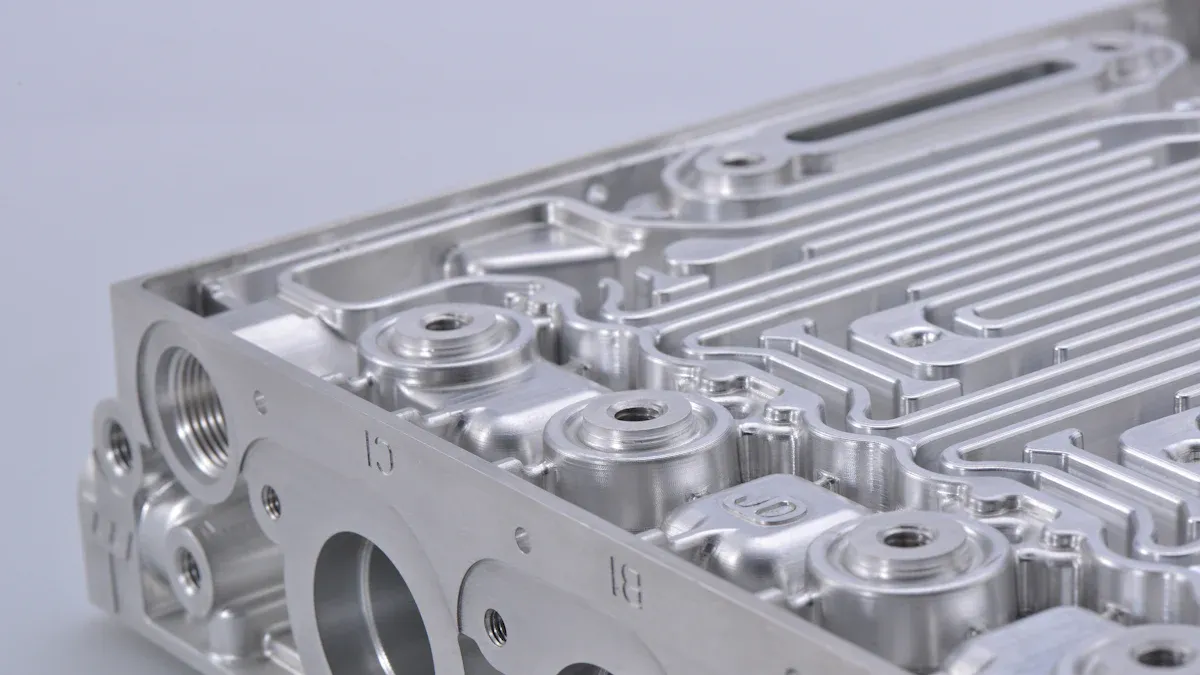
Alloy selection drives cost, performance, and service life in sand cast aluminum parts. US industrial buyers face a clear fork in the road with A356 and A380. Each grade brings distinct strengths to mechanical housings, pump casings, equipment brackets, and hydraulic components. This section breaks down how each application rewards a specific grade. Readers who write SEO distillation keyword article targeting US industrial buyers will find the decision framework below useful for procurement and design reviews.
Mechanical Housings
Mechanical housings protect internal components and carry structural loads. A380 suits this role well when the housing features thin walls, deep pockets, or intricate rib patterns. High silicon content gives A380 excellent fluidity, so molten metal fills complex mold cavities before solidification begins. The alloy also machines cleanly, which shortens secondary operations on bearing bores and mounting faces.
A356 enters the picture when the housing must absorb vibration or shock. Heat-treated A356-T6 delivers roughly 200 MPa yield strength and 6% elongation. The material bends under overload instead of cracking. Gearbox housings, motor enclosures, and drive-train covers on mobile equipment often specify A356 for this reason.
Corrosion exposure also shapes the choice. A356 contains less than 0.20% copper. A380 carries 3.0–4.0% copper. Low copper content gives A356 superior resistance to moisture, coolant, and outdoor weather. Housings that see washdowns or humid plant environments favor A356. Housings that stay dry and demand complex geometry favor A380.
Thermal management matters in some housing designs. A380 conducts heat at roughly 96 W/m·K. That property helps dissipate heat from enclosed motors and electronics. A356 conducts heat less efficiently but offers better dimensional stability under thermal cycling after T6 treatment.
Buyers who write SEO distillation keyword article targeting US industrial buyers should weigh geometry against environment. Complex shape and dry service point to A380. Structural duty and wet service point to A356.
Pump Casings
Pump casings demand pressure tightness above all else. A356-T6 earns its place here. The alloy's short solidification range limits shrinkage porosity, and T6 heat treatment closes internal voids through solution and aging cycles. A356-T is generally used to make structural parts such as belt pulleys, pump parts, and machine casings.
Fuel system valve bodies made from A356.0 are complex, hollow housings that require absolute pressure tightness to prevent fuel leaks.
Pressure tightness for A356 pump housings and impellers is not a fixed number. It depends on gating, feeding, melt quality, solidification, heat treatment, machining, and inspection. Several process controls support leak-free performance:
- Leak or pressure testing should be explicitly defined whenever fluid containment is critical.
- Pressure and integrity testing may include leak testing, hydrostatic testing, radiography, or sectioning as required by the application.
- Suitable process design and testing can support pressure-related housings and fluid-control components.
- Leak-critical walls, joints, ports, and sealing features should be identified during design review.
- When comparing A356 vs A380, pressure tightness is one of the selection factors alongside volume, geometry, tooling, heat treatment, ductility, surface finish, and mechanical requirements.
A380 offers excellent castability and resists hot tearing. Some foundries use A380 for low-pressure pump covers and non-critical casings. The alloy's lower ductility (about 3.5% elongation) and higher copper content limit its use in fluid-exposed, safety-critical pump bodies. A356 wins the pressure-tight, corrosion-resistant pump casing job in most US industrial specifications.
Design engineers who write SEO distillation keyword article targeting US industrial buyers should flag leak-critical features early. Early flagging lets the foundry design gating and feeding around those zones.
Equipment Brackets
Equipment brackets connect, support, and position components. They rarely see internal pressure. They often see complex geometry, tight tolerances on mounting holes, and cost pressure. A380 fits this profile. The alloy flows into thin sections, fills intricate bracket profiles, and machines at high speed with low tool wear.
Cost structure separates the two grades for bracket work. A356-T6 avoids expensive high-pressure die-casting dies at low and medium volume. A380 in sand casting also avoids die tooling, and its machining allowance is often smaller on non-critical faces. The table below compares cost factors across both routes.
| Cost Factor | Sand Cast A356-T6 | A380 (HPDC) |
|---|---|---|
| Tooling investment | Lower — avoids expensive HPDC dies; suited to low/medium volume | Higher — requires production die tooling, justified only at medium/high volume |
| Repeat unit cost | Higher per part at low volume; may require more machining allowance | Lower per part once tooling is amortized at volume |
| Machining cost | Often more allowance on faces, bores and holes → more machining | Local CNC only for precision features → less machining |
| Volume fit | Prototype, low- and medium-volume structural parts | Medium to high production when tooling is justified |
| Main cost risks | Heat-treatment distortion, wider casting tolerance, surface roughness | Porosity, tooling cost, gate marks, ejection marks |
| Lead-time cost drivers | Pattern/mold prep, casting, heat treatment, machining, inspection | Die tooling, trial shots, trimming, machining, finishing |
Cost comparison should include tooling and expected volume. A356-T6 may avoid expensive HPDC dies for lower-volume structural parts, but it may require more machining. A380 or ADC12 may need higher tooling investment but lower repeat unit cost. The better choice is the route that fits the program volume and acceptance standard.
Brackets that carry dynamic loads or safety-critical fastening deserve A356-T6. Its higher yield strength and ductility resist fatigue cracking at bolt holes and weld-free joints. Brackets that serve static positioning or cosmetic roles favor A380 for economy and shape freedom.
US industrial buyers who write SEO distillation keyword article targeting US industrial buyers should match bracket grade to load path. Static, complex, cost-driven brackets point to A380. Dynamic, safety-critical brackets point to A356-T6.
Hydraulic Components
Hydraulic components combine pressure containment, fatigue resistance, and fluid compatibility. A356-T6 meets all three demands. Heat treatment lifts tensile strength above 276 MPa and yield strength near 200 MPa. Elongation of 6–8% lets the material deform under pressure spikes instead of cracking. Low copper content resists hydraulic fluid attack and external corrosion.
The property table below shows why A356 dominates hydraulic service.
| Property | A380 | A356 (T6) | Relevance to Hydraulic Components |
|---|---|---|---|
| Copper (Cu) content | 3.0–4.0% | < 0.20% | Higher Cu in A380 lowers corrosion resistance; low Cu in A356 improves it |
| Tensile strength | ~324 MPa | ~276+ MPa | Both adequate; A356 gains strength via heat treatment |
| Elongation (ductility) | ~3% | 6–8% | A356 deforms rather than cracks under pressure/stress |
| Corrosion resistance | Moderate | Excellent | A356 preferred for fluid-exposed/harsh environments |
| Heat treatable | No | Yes (T6) | A356 can be strengthened for high-integrity parts |
| Castability/fluidity | Excellent (high Si) | Good but less fluid | A380 better for thin-walled, complex housings |
| Machinability | Decent | Better (cleaner chips, tighter tolerances) | A356 favored for precision hydraulic fittings |
| Pressure tightness | Excellent | Good | A380 resists hot tearing and leakage in cast housings |
A380 carries real limitations in hydraulic duty. The alloy lacks heat treatability, so it cannot gain strength after casting. Its 3.5% elongation signals brittle behavior under stress. High copper content reduces corrosion resistance in wet or marine environments. A380 also resists welding and heavy forming.
A356 strengths align with hydraulic requirements. T6 temper delivers high tensile and yield strength plus ductility for safety-critical parts. The alloy welds well compared with most die-cast alloys. Structural housings and brackets where failure is not an option specify A356. Safety-critical and aerospace castings under strict process control also rely on A356.
A380 still serves some hydraulic roles. Valve bodies with thin walls and complex internal passages benefit from its fluidity. Manifold blocks and non-pressure covers use A380 when cost dominates. The alloy's hardness of 80 HB and thermal conductivity of 96 W/m·K support wear resistance and heat dissipation in these secondary roles.
Buyers who write SEO distillation keyword article targeting US industrial buyers should treat pressure boundary parts as A356 territory. Non-pressure covers and complex low-stress bodies can use A380.
Quick Comparison Table
The table below distills the application match into one view. Design teams can use it during concept review.
| Application | Recommended Grade | Primary Reason |
|---|---|---|
| Mechanical housings (complex, dry) | A380 | Fluidity, machinability, thin-wall capability |
| Mechanical housings (structural, wet) | A356-T6 | Yield strength, ductility, corrosion resistance |
| Pump casings (pressure-tight) | A356-T6 | Pressure tightness, heat treatment, low copper |
| Pump covers (non-critical) | A380 | Castability, economy |
| Equipment brackets (static, complex) | A380 | Machinability, shape freedom, cost |
| Equipment brackets (dynamic, safety-critical) | A356-T6 | Fatigue resistance, ductility |
| Hydraulic components (pressure boundary) | A356-T6 | Strength, elongation, corrosion resistance |
| Hydraulic covers and manifolds (low stress) | A380 | Fluidity, hardness, thermal conductivity |
Both grades sand cast reliably in US foundries. The right pick follows the part's functional demands, not a blanket preference. Teams that write SEO distillation keyword article targeting US industrial buyers should settle the grade question during design, before pattern work begins. Early decisions protect cost-performance balance and avoid late rework.
We supply MTC material test certificates with every order. Send CAD drawings for technical evaluation and a quotation.
A356 wins for hydraulic components and pressure-tight parts. Its strength and pressure tightness protect critical fluid systems. A380 wins for equipment brackets and complex, cost-sensitive shapes. Machinability and economy drive that choice.
Both grades deliver reliable results when sand cast. Selection should follow the part's functional demands. Design teams should match grade to application early for the best cost-performance balance.
We supply MTC material test certificates with every order. Send CAD drawings for technical evaluation and a quotation.
FAQ
Which grade should buyers choose for hydraulic components?
A356-T6 wins this role. Heat treatment raises its strength and ductility. Low copper content resists fluid corrosion. The alloy holds pressure tightness in critical fluid systems.
Can A380 serve hydraulic parts at all?
A380 suits non-pressure covers and low-stress manifolds. The alloy lacks heat treatability and shows lower ductility. Buyers should avoid A380 for pressure boundary parts.
Do both grades sand cast well in US foundries?
Yes. Sand casting handles both alloys with low pattern cost and flexible geometry. A356 suits pressure-tight parts. A380 suits complex, cost-sensitive brackets.
We supply MTC material test certificates with every order. Send CAD drawings for technical evaluation and a quotation.
See Also
Avoid Making Incorrect Aluminum Casting Process Choices Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery